1. Presentation of results (before and after comparison)
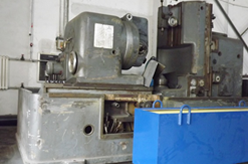 | 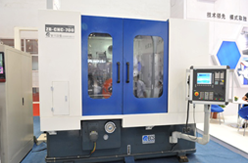 |
| Before remanufacturing ZB700 | ZB700 after remanufacturing |
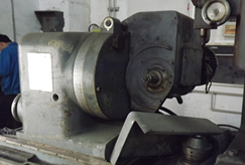 | 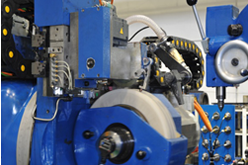 |
| Before remanufacturing of ZB700 grinding wheel carrier | ZB700 Grinding Wheel Holder after remanufacturing |
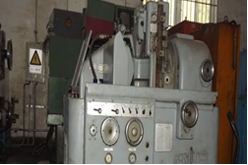 | 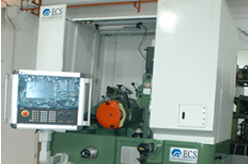 |
| Before remanufacturing of NZA worm grinding machine | Post remanufacturing of NZA worm grinding machine |
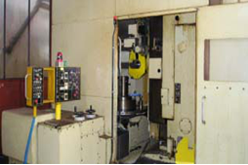 | 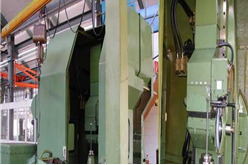 |
| Before remanufacturing of 7NILES1500 gear grinding machine | NILES1500 gear grinding machine after remanufacturing |
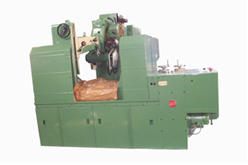 | 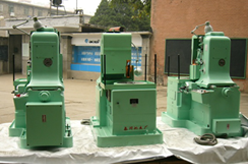 |
| Y7163 after reconstruction | Y7654 after reconstruction |
 | 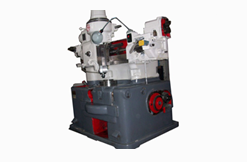 |
| Y7150 after reconstruction | Manufactured Y54 |
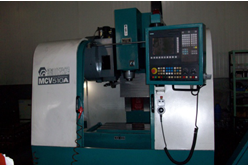 |  |
| Modified NCV510 | Reconstructed HOFLOR630 |
Sharing of remanufacturing process of worm grinding wheel grinding machine:
Grinding wheel frame part: the grinding wheel frame part adopts the foreign large inertia motor directly connected to drive the grinding wheel gear grinding machine, so as to realize the light, stable and reliable operation speed control (0-2000 rotation adjustment) of the spindle system. The finishing part adopts the servo motor and high-precision speed reduction machine, which can easily form the double-head to multi-head grinding wheel.
Workpiece frame part: in the first part, the main shaft support of the workpiece frame adopts the high-precision rolling bearing support structure, so that the rigid structure and bearing capacity of the workpiece main shaft are greatly improved; The second part adopts the primary gear reduction, and the servo motor directly drives the workpiece spindle to carry out precise and non-backlash rotation movement, providing a short and reliable transmission chain platform for precision grinding.
Hydraulic system: the first part is the drive of workpiece frame movement (Z-axis), which uses the linear motor drive principle, and uses the electro-hydraulic linear motor drive module to control the electro-hydraulic proportional valve and drive the hydraulic cylinder. In the second part, the position feedback adopts high-precision long grating feedback, which makes the Z-axis movement more stable and reliable, and the moving speed is infinitely adjustable. The upper and lower and middle stop positions are reliably controlled in real time, providing support for high-precision grinding.
Electrical control system: Siemens 840D system is adopted for control, and tooth direction numerical control shaping function can be added; Continuous tangential displacement grinding function, etc. It really realizes 5-axis linkage control, Z-axis and Y-axis (tangential displacement axis) high-precision follow-up, and achieves the purpose of precise gear grinding. X-axis (grinding wheel rack feed shaft). It can be interpolated along with the movement of axis Z, so as to realize any CNC gear direction repair. The NC modified worm wheel can realize the easy shaping of double-head or 3-head grinding worm, and the high efficiency and high precision grinding of gear workpiece with multiple teeth and small modulus can be realized economically.
2. Classic case analysis
Case 1:
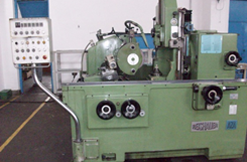
Before remanufacturing of AZA worm grinding machine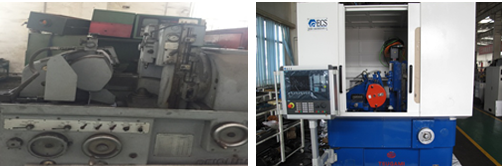
Remanufactured AZA worm grinding machine
Before remanufacturing:
1. Grinding wheel finishing and workpiece grinding require the installation of exchange coupling, long transmission chain, complex coupling calculation, large error and low processing efficiency.
2. No multi-head grinding wheel grinding function.
3. Tangential displacement is manual.
4. The hydraulic system is non-standard and placed in the machine.
5. The grinding wheel spindle is of sliding bearing structure.
6. Modulus: 0.5-6 Teeth: 12-256
7. Level 7 machining accuracy.
Following remanufacturing:
1. Siemens 840D numerical control system 6-axis servo control is adopted to cancel the original machine tool modulus, split teeth, differential exchange coupling, shorten the transmission chain to reduce transmission error and improve the processing efficiency.
2. Realize automatic trimming of tooth shape and excircle of any modulus of grinding wheel; Automatic trimming of multi-head grinding wheel; Multi-head grinding wheel grinding;
3. Continuous displacement grinding; NC gear direction shaping; Automatic grinding cycle; Manual grinding cycle.
4. The standard hydraulic component external liquid station is adopted for the convenience of maintenance and repair.
5. Grinding wheel and workpiece spindle are of rolling bearing structure, which is convenient for maintenance.
6. Modulus 0.2-6 Teeth: 7-300
7. The machining accuracy can be stabilized at Level 5, and some accuracy can reach Level 3.
8. Processing efficiency improved by 50% compared to remanufacturing.
9. Equipped with full protective cover and static point mist absorption device.
Case 2:
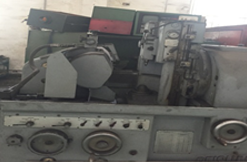 | 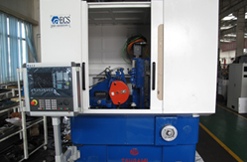 |
| Japanese T-G300 before remanufacturing | Japan T-G300 after remanufacturing |
Japanese T-G300 worm grinding machine
Before remanufacturing:
1. Grinding wheel finishing and workpiece grinding require the installation of exchange coupling, long transmission chain, complex coupling calculation, large error and low processing efficiency.
2. No automatic grinding cycle, no multi-head grinding wheel grinding function.
3. Tangential displacement is manual.
4. The hydraulic system is non-standard and placed in the machine.
5. The grinding wheel spindle is of sliding bearing structure.
6. Modulus: 0.5-5 Teeth: 12-256
7. Level 7 machining accuracy.
Following remanufacturing:
1. Siemens 840D numerical control system 6-axis servo control is adopted to cancel the original machine tool modulus, split teeth, differential exchange coupling, shorten the transmission chain to reduce transmission error and improve the processing efficiency.
2. Realize automatic trimming of tooth shape and excircle of any modulus of grinding wheel; Automatic trimming of multi-head grinding wheel; Multi-head grinding wheel grinding;
3. Continuous displacement grinding; NC gear direction shaping; Automatic grinding cycle; Manual grinding cycle.
4. The standard hydraulic component external liquid station is adopted for the convenience of maintenance and repair.
5. Grinding wheel and workpiece spindle are of rolling bearing structure, which is convenient for maintenance.
6. Modulus 0.2-6 Teeth: 7-300
7. The machining accuracy can be stabilized at Level 5, and some accuracy can reach Level 3.
8. Processing efficiency improved by 50% compared to remanufacturing.
9. Equipped with full protective cover and static point mist absorption device.